 Spanish
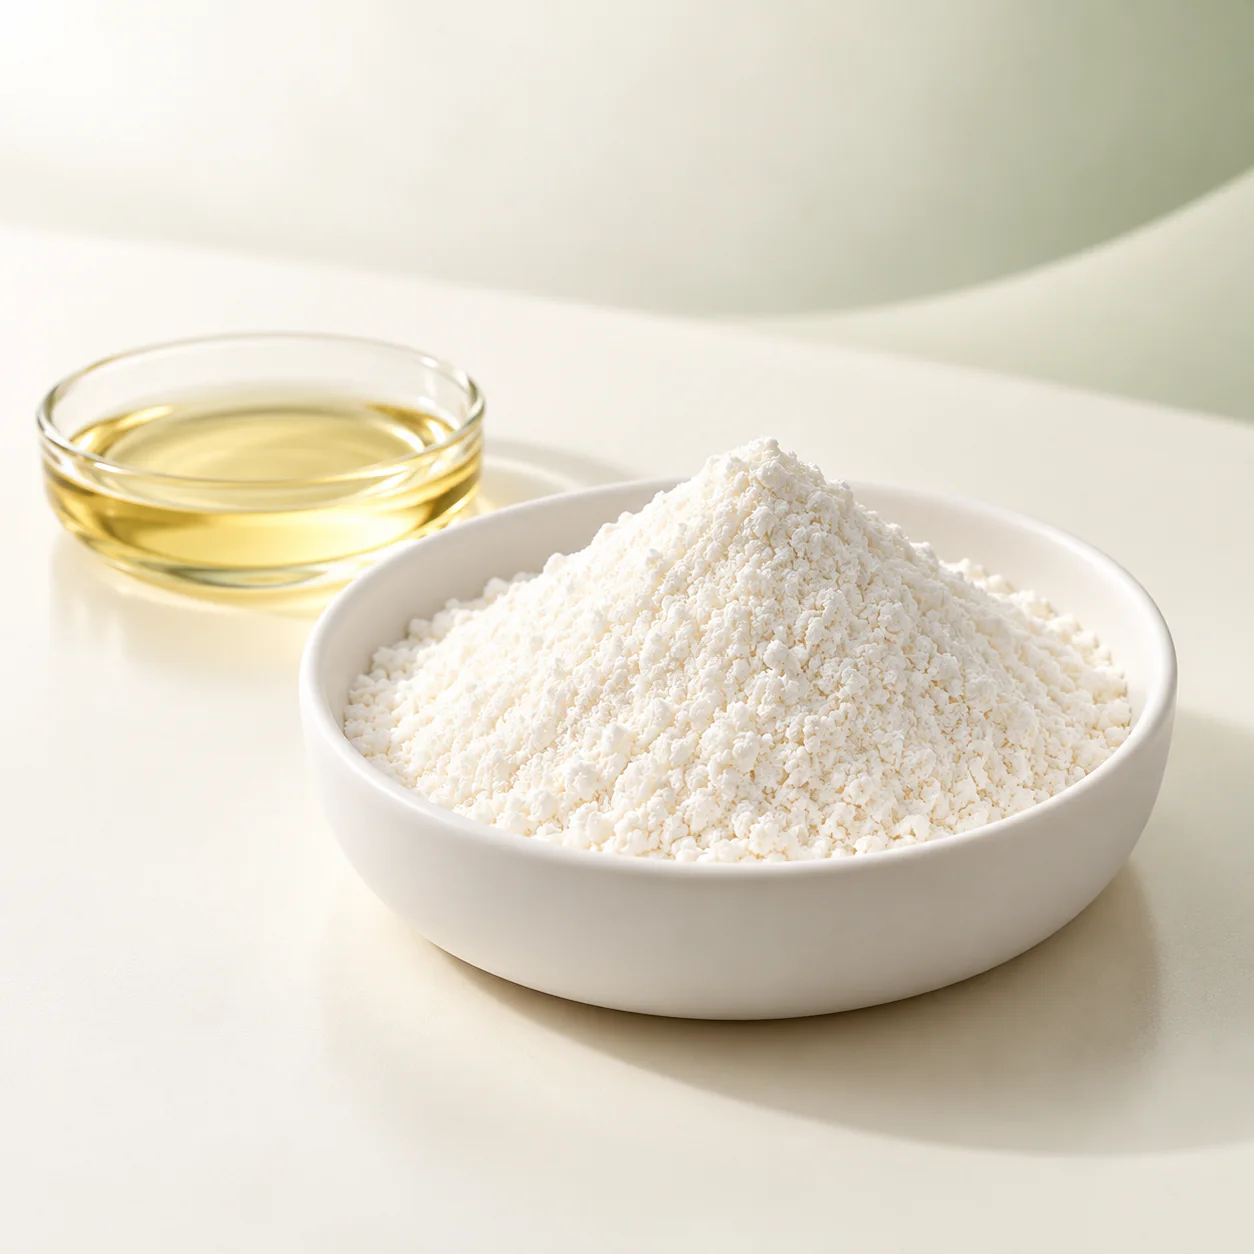
Ureda Naturals is a Gamma Oryzanol manufacturer supplying high-assay material for dietary supplements, softgel fills and oil-phase personal-care formulations. The standard powder is controlled at 97.0%–103.0% by UV and supported by identity, residual-solvent, heavy-metal and microbiological testing.
| Product Name | Gamma Oryzanol |
|---|---|
| CAS NO: | 11042-64-1 |
| Appearance | White or almost white Powder |
| Specification | 97.0%–103.0% |
| Packaging | 20 kg/drum |
Ureda Naturals manufactures and supplies high-assay Gamma Oryzanol Powder for dietary supplement, lipid-based product and personal-care manufacturing. The standard powder is controlled at 97.0%–103.0% by UV, with identity, residual-solvent, heavy-metal and microbiological testing included in the quality specification.
This grade is insoluble in water. It is primarily intended for controlled dry blending, oil-phase incorporation and properly designed emulsified systems. Water-based products require a separately developed dispersible delivery format.
The standard high-assay powder is suitable when the formulation route can accommodate a water-insoluble ingredient.
A standard powder and a water-dispersible grade are not direct substitutes. A dispersible product normally contains a carrier or delivery system, so its active loading, processing behavior and assay basis must be evaluated separately.
Gamma Oryzanol is a group of ferulic-acid esters formed from plant sterols and triterpene alcohols. Common constituents include cycloartenyl ferulate, 24-methylenecycloartanyl ferulate and campesteryl ferulate.
It is not a single purified molecule. Commercial quality should therefore be evaluated through total Gamma Oryzanol assay, chemical and spectroscopic identity, solubility, moisture, inorganic residue, residual solvents, heavy metals and microbiological quality.
Two products carrying similar assay values may still behave differently during blending, oil-phase incorporation, emulsification or cooling. Assay is essential, but it is not a complete prediction of manufacturing performance.
| Selection Point | Standard High-Assay Powder | Water-Dispersible Format |
|---|---|---|
| Primary Objective | High active concentration | Improved dispersion in aqueous systems |
| Typical Composition | Predominantly active powder | Active combined with a carrier or delivery system |
| Typical Applications | Capsules, tablets, dry premixes, oil phases, softgels, balms and emulsions | Beverages and other water-dominant products |
| Water Behavior | Insoluble | Depends on the carrier and delivery technology |
| Assay Interpretation | Based on the high-assay powder specification | Must account for carrier content and active loading |
| Manufacturing Focus | Blend uniformity, oil compatibility and crystallization control | Dispersion stability, sedimentation and active uniformity |
| Interchangeability | Not directly interchangeable | Not directly interchangeable |
| Test Item | Specification | Result | Method |
|---|---|---|---|
| Appearance | White or almost white powder; odorless | White powder; odorless | Visual and sensory |
| Solubility | Soluble in acetone; slightly soluble in n-heptane; insoluble in water | Conforms | In-house method |
| Chemical Reaction | Positive | Positive | Chemical test |
| UV Spectrum | Complies with reference spectrum | Complies | UV |
| Test Item | Specification | Result | Method |
|---|---|---|---|
| Assay | 97.0%–103.0% | 100.9% | UV |
| Loss on Drying | ≤0.8% | 0.2% | ChP 2025 |
| Residue on Ignition | ≤0.2% | 0.04% | ChP 2025 |
| Methanol | ≤0.1% | <0.1% | GC |
| Test Item | Specification | Result | Method |
|---|---|---|---|
| Heavy Metals | ≤10 mg/kg | <10 mg/kg | ChP 2025 |
| Arsenic | ≤2 mg/kg | <2 mg/kg | ChP 2025 |
| Total Aerobic Microbial Count | ≤1,000 CFU/g | <10 CFU/g | ChP 2025 |
| Yeasts and Molds | ≤100 CFU/g | <10 CFU/g | ChP 2025 |
| Escherichia coli | Negative in 1 g | Negative | ChP 2025 |
The assay specification is 97.0%–103.0% by UV. The reported value is calculated against the selected reference standard under the specified analytical conditions.
A product reported as 98% by HPLC cannot be ranked directly against a product reported as 97.0%–103.0% by UV. Before comparing results, align the definition of total Gamma Oryzanol, analytical method, reference standard, component coverage, calculation basis and any moisture correction.
HPLC can provide separated component information, while UV measures the total response under the defined release method. Different numerical results do not automatically indicate a genuine difference in ingredient quality.
A passing assay establishes concentration under the selected method, but product approval should also include identity confirmation. Chemical reaction and UV-spectrum conformity strengthen the incoming-quality assessment when reviewed with appearance, assay and solubility.
Methanol is controlled at not more than 0.1% by GC. When the target market or customer specification requires additional residual-solvent controls, the required solvent list and limits should be included in the purchasing specification before commercial approval.
| Finished Product | Development Approach | Primary Risk | Approval Check |
|---|---|---|---|
| Hard Capsules | Prepare a staged preblend before the main blend | Segregation at low inclusion levels | Blend and capsule content uniformity |
| Tablets | Pre-dilute with a compatible carrier | Uneven distribution or changes in flow | Final blend assay and compression performance |
| Dry Premixes | Produce a controlled lower-concentration premix | Localized concentration and sampling error | Multi-point sampling |
| Softgels | Develop as a verified solution or suspension | Sedimentation or crystallization during holding | Fill uniformity and early-to-late capsule assay |
| Facial and Body Oils | Introduce through a compatible oil phase | Incomplete dissolution or crystals after cooling | Clarity and storage stability |
| Balms and Sticks | Incorporate into the heated lipid phase | Graininess or crystal growth | Texture and cooling stability |
| Creams and Lotions | Incorporate through the oil phase before emulsification | Crystallization after emulsification | Microscopic appearance and emulsion stability |
| Water-Based Products | Use a separately developed dispersible system | Floating, sedimentation and dose inconsistency | Physical stability and analytical uniformity |
Gamma Oryzanol may represent only a small proportion of a capsule or tablet formula. Adding it directly to a full-size blender can create concentrated areas that are difficult to correct.
The final check is important because a blend can be uniform immediately after mixing and still segregate during discharge, vibration, transfer or hopper residence. When content uniformity fails, investigate particle and density differences, preblend ratio, mixing sequence, transfer conditions and hopper holding. Increasing mixing time alone may not solve segregation.
Gamma Oryzanol is lipophilic, but it should not be assumed to dissolve completely in every oil at the intended concentration. Its behavior depends on the oil system, active concentration, other dissolved ingredients, processing temperature, holding time, cooling profile and storage temperature.
A heated oil phase may initially appear clear because solubility is temporarily higher. During cooling, the system can become supersaturated and form haze, sediment or crystals. A hot, transparent mixture is therefore not sufficient evidence of finished-product stability.
Evaluate the system at the processing and filling temperatures, after complete cooling, after 24–48 hours and at the expected room and lower storage temperatures. Compare active distribution between the upper and lower portions of the vessel when sedimentation is possible.
For a solution fill, confirm that Gamma Oryzanol remains dissolved through preparation, holding, encapsulation and storage. For a suspension fill, control particle size, vehicle viscosity, agitation, sedimentation and maximum holding time. Compare capsules collected at the beginning, middle and end of production to identify concentration drift.
Introduce the standard powder through a compatible oil phase before emulsification. Complete oil-phase incorporation does not guarantee that the ingredient will remain dissolved after water-phase addition. Emulsification, dilution and cooling can change the solvent environment and initiate crystal formation.
Evaluate the oil phase before emulsification, crystal formation during cooling, microscopic appearance after storage, viscosity, phase stability and Gamma Oryzanol distribution. Filtering visible particles is not automatically corrective: removing crystallized active can improve appearance while lowering the actual active concentration.
The standard powder is insoluble in water and should not be added directly to an aqueous product as though it were an instant powder. Direct addition can cause floating, incomplete wetting, deposits, sedimentation and non-uniform dosing.
Water-based applications require a separately developed emulsified, encapsulated or otherwise dispersible format. Test the selected system under the actual pH, ionic strength, heat treatment and storage conditions. Measure both physical stability and Gamma Oryzanol content uniformity; visual appearance alone is not sufficient.
Gamma Oryzanol can contribute to an antioxidant formulation strategy, but its inclusion does not by itself establish finished-product shelf life. Final stability depends on the complete formulation, manufacturing process and commercial package.
Use the lowest effective processing temperature and shortest practical holding period required for incorporation. Evaluate assay retention, haze or crystals, sediment, color and odor change, relevant lipid-oxidation markers, physical stability and package compatibility in the final formulation.
Two products described as “98% Gamma Oryzanol Powder” should not be approved as interchangeable solely from the headline assay. Align product identity, assay range, analytical method, reference standard, calculation basis, solubility, moisture, residue, residual-solvent controls, heavy-metal limits and microbiological specifications.
When changing suppliers, compare both materials in the same formula and process. Depending on the dosage form, evaluate blend uniformity, oil-phase compatibility, cooling and crystallization behavior, suspension stability, finished-product assay and stability. A matching incoming assay confirms only one part of equivalence.
To match the ingredient and documentation to the intended project, provide:
For water-based development, specify whether the target is a clear solution, stable emulsion or suspended system. This determines whether the standard high-assay powder is suitable or a separate delivery format is required.
Store in the original sealed package in a cool, dry place. Protect from direct light, heat and moisture. After opening, use clean and dry dispensing equipment, minimize exposure during weighing, reseal the remaining material promptly and retain the original batch identification.
Available quality support includes the Certificate of Analysis, product specification, Technical Data Sheet, Safety Data Sheet and applicable quality, regulatory and supply-chain documentation. GMP, FSSC 22000, ISO 9001, HACCP, Halal and Kosher documentation is available according to the applicable product, purchasing and market requirements.
The result is calculated against a reference standard under the specified UV method. It is not a direct statement that the powder contains more than 100% physical material. Analytical and reference-standard variation is controlled through the 97.0%–103.0% release range, so a result of 100.9% complies with specification.
Not unless the product definition, reference standard, calculation basis and component coverage are aligned. UV measures total response under the specified release method, whereas HPLC separates chromatographic components before calculation. Different methods can generate different numerical results from the same material.
No. A dispersible format normally contains a carrier, emulsifier, encapsulation system or other delivery technology. Its active concentration and processing behavior differ from the standard high-assay powder, so the two formats require separate specifications and formulation validation.
Assay does not describe every physical or compositional attribute that affects processing. Differences in particle characteristics, component distribution and compatibility with the selected carrier can alter blending, suspension behavior and crystallization.
The specification should define identity, assay range, method, reference standard, calculation basis, solubility, loss on drying, residue on ignition, relevant residual solvents, heavy metals, microbiological limits, packaging and storage. Add application-specific physical requirements separately when they affect manufacturing performance.
First align the specification and analytical methods. Then compare both materials in the intended formula and process. Depending on the dosage form, verify blend uniformity, oil compatibility, crystallization, suspension stability, finished-product assay and stability. Similar incoming assay results alone do not establish process equivalence.
INGREDIENT PARTNER
Tell us your intended application, approximate quantity and target market. Ureda Naturals will confirm the closest grade, packaging configuration and available documentation for your project.
Scan the QR code or
search WeChat ID: 18270717590
From Natural Origin to Formulation Intent
Tell us what you’re sourcing.